Jinye Machinery
Pallet stability is not created by film alone. It depends on load design, product friction, pallet quality, and consistent machine settings. How to optimize pallet stability using stretch hood technology begins with observing the complete packaging system. A beverage pallet may need different containment than cartons with smooth, dusty surfaces. Uneven layers, crushed corners, and excess overhang can create movement before the hood is applied. Small details matter. Operators should check pallet dimensions, load height, film elasticity, and gripping force during routine production. They should also inspect film tension at the pallet’s top, sides, and lower edge. Excessive tension may damage cartons, while weak containment allows shifting. The correct balance is rarely achieved through guesswork.
Practical validation should include warehouse handling and transport simulations. Measure pallet movement after forklift transfers, vibration exposure, and controlled tilt testing. Compare results across different film gauges and hood sizes. Record failures with photographs, not assumptions. A stable pallet should remain aligned without crushed packaging or exposed products. Machine calibration, clean film paths, and regular maintenance support repeatable performance. Manufacturer recommendations and applicable packaging safety standards should guide the final settings. Experience shows that one successful trial does not prove long-term reliability. Humidity, temperature, product weight, and operator habits can change results. That is easy to overlook. Continuous review is necessary. By combining measurable tests with trained observation, companies can improve load security, reduce rework, and develop a stretch hood process that performs reliably in real distribution conditions.
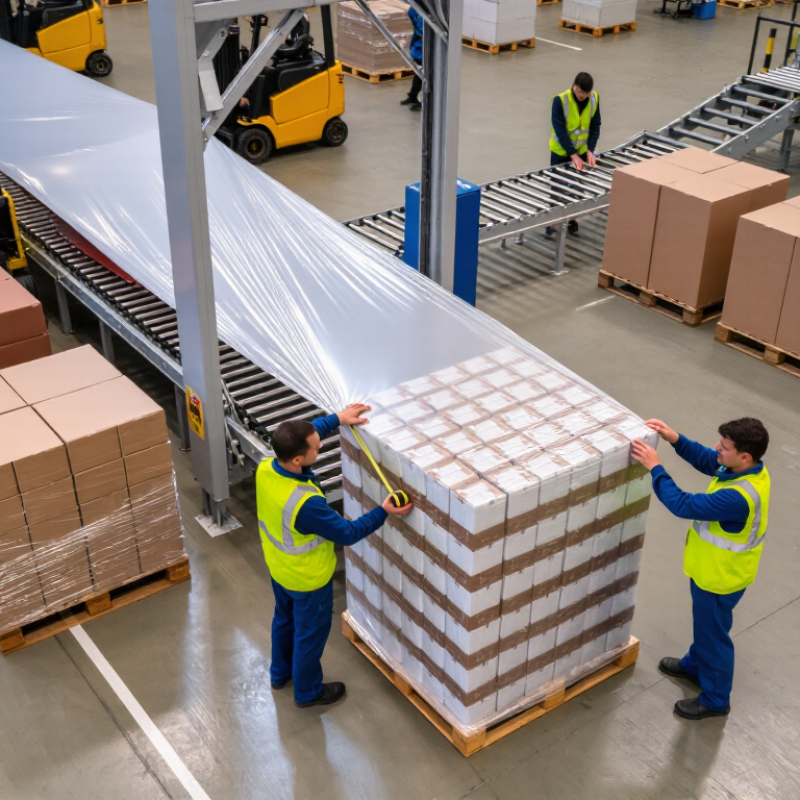
Pallet stability begins with the load, not the stretch hood. A stable pallet has a low center of gravity, even weight distribution, and aligned cartons. Heavy cases should sit below lighter ones. Gaps between boxes create movement during braking, turning, and vibration. Real pallets are rarely perfect.
A stretch hood works by extending elastic film over the load and letting it contract around the sides. The film should grip the pallet without crushing cartons or bending corners. Correct sizing matters. Excess film may create weak folds, while insufficient film can expose the upper layers. Corner protectors can reduce pressure on sharp carton edges. The bottom seal should sit below the pallet deck when possible.
During inspections, check loose layers, film tears, tilted cartons, and uncovered pallet edges. Look closely at the first and last pallet from each production run. Small changes in carton moisture, temperature, or product weight can affect holding force. Film performance also changes in cold storage. This is easy to overlook.
I have found that excessive tension is not always better. It can distort boxes and hide poor stacking. A simple tilt test may reveal movement, but it cannot replace transport trials. Measure the load after wrapping, after handling, and after storage. Record the film width, applied tension, pallet height, and visible damage. Some results will be disappointing. That is useful evidence.
A stable pallet begins with the load, not the film. Measure pallet width, height, weight, and center of gravity before selecting a stretch hood. Mixed cartons, uneven layers, and soft bags create different movement patterns. A tall pallet with a narrow base needs stronger vertical restraint. A dense, low pallet may need less material, but it still requires edge protection.
EUMOS 40509 evaluates load stability under horizontal acceleration of up to 0.5 g. This figure exposes weak patterns that look stable inside a warehouse. ISTA 3E also combines vibration, compression, and handling impacts during distribution testing. Use these tests when shipments face forklifts, ramps, or long-distance vibration.
In practical trials, inspect corner displacement and carton deformation after testing. I once treated a light pallet as low risk. It shifted badly. Weight alone misleads.
Tips: Record the heaviest and weakest load patterns. Match hood width to the widest footprint. Choose higher elasticity for irregular loads. Avoid excessive tension around crush-sensitive cartons. Confirm performance after cold storage, because low temperatures can reduce film flexibility.
Select the hood by restraint need, not only by thickness. The correct design should hold the top layer, protect the load from dust, and remain open at the base when required. Industry testing should guide the setting, but warehouse observations matter too. A perfect laboratory result can still fail on a rough loading route. Recheck the pallet after real transport.
How to Optimize Pallet Stability with Stretch Hood in 2026?
Preparing a pallet correctly begins before the stretch hood reaches the load. Inspect the pallet deck for broken boards, moisture, and loose nails. A damaged base can shift under pressure. Keep heavier cartons low, and place lighter packages above them. Align every layer with the pallet edges. Small gaps can become movement points during transport. Keep the load centered, with its weight distributed across the full deck. Avoid overhanging cartons unless the packaging specification allows it. Secure irregular items with suitable inner supports. Clean, dry surfaces also improve film contact.
Alignment matters more than appearance. Check vertical corners from the pallet floor to the top layer. They should form stable lines, not leaning towers. Press gently against each side and look for rocking. Rocking means the load needs adjustment before hooding. During production checks, measure the load height and width, then select a hood with enough clearance. Too little clearance may tear the film. Too much can reduce containment. I have seen neat pallets fail because one bottom carton was crushed. It looked minor. It was not. After hooding, inspect the lower seal area and confirm that the film reaches evenly around the pallet. Test sample loads under vibration or braking conditions when possible. Real movement reveals weaknesses that visual checks miss. The process is reliable, but it is not automatic. Teams should record failures and revise loading patterns regularly.
| Process Stage | Control Dimension | Recommended Target or Range | Verification Method | Stability Benefit |
|---|---|---|---|---|
| Pallet selection | Pallet condition | Dry, clean, structurally sound; no protruding nails, broken boards, or severe deck-board deformation | Visual inspection before loading; reject damaged pallets | Prevents film puncture, load tilt, and uneven support at the pallet base |
| Pallet selection | Pallet footprint compatibility | Load footprint should be compatible with the pallet deck; avoid excessive unsupported overhang | Measure the load and pallet length and width at receiving or packing | Reduces edge collapse and improves vertical load transfer |
| Product preparation | Product alignment | Keep cartons square to the pallet edges; align vertical faces and avoid staggered protrusions | Check two adjacent sides and the top layer before hood application | Creates consistent film contact and limits lateral movement |
| Product preparation | Layer interlock and column pattern | Use a repeatable stacking pattern; avoid unsupported corners, unstable partial layers, and excessive gaps | Review the pallet pattern against the approved packing layout | Improves compression transfer and reduces carton shifting during handling |
| Load geometry | Pallet squareness | Keep the load centered and square; visible skew should be corrected before packaging | Measure diagonal or corner-to-corner differences on the load footprint | Prevents uneven hood tension and corner loading |
| Load geometry | Center of gravity | Keep the center of gravity as low and central as practical; place heavier products in lower layers | Review product weights and stacking sequence | Reduces tipping risk during acceleration, braking, and cornering |
| Load geometry | Top-surface uniformity | Avoid sharp height changes, loose top cartons, and exposed product edges where possible | Inspect the top layer before the hood is opened | Helps the hood settle evenly and limits local stress concentrations |
| Surface protection | Sharp-edge protection | Use suitable corner boards, edge protectors, or smooth protective sheets at puncture-prone locations | Check corners, straps, bands, and exposed edges manually | Prevents film tearing and distributes hood tension over vulnerable areas |
| Load restraint | Use of bands or strapping | Use only when required by the load design; secure unstable units before applying the stretch hood | Confirm strap tension, placement, and edge protection | Provides initial restraint for loads that cannot be stabilized by film alone |
| Film selection | Film thickness | Select thickness according to load weight, geometry, puncture risk, and transport conditions; common industrial ranges are approximately 40–120 micrometres | Confirm the film technical data sheet and perform a trial pack | Balances puncture resistance, containment force, and material consumption |
| Film selection | Film width and hood dimensions | Match the hood width and length to the pallet footprint and total load height without excessive loose film | Use load dimensions plus the film supplier’s sizing method | Improves coverage from the pallet base to the load top |
| Machine setup | Film centering | Keep the film centered across the load; left and right side coverage should be visibly balanced | Inspect film position and hood travel during the first packs of each changeover | Prevents asymmetric restraint and uneven corner tension |
| Machine setup | Hood application height | Position the hood to cover the full load and engage the pallet area as specified by the packaging-machine setup | Verify bottom coverage and top clearance on sample pallets | Improves vertical hold-down force and reduces film lift |
| Machine setup | Film tension and sealing or shrink parameters | Use the film manufacturer’s validated operating window; avoid excessive tension, overheating, or under-shrinkage | Inspect for tears, loose panels, burn marks, and inconsistent contraction | Maintains containment without damaging products or weakening the film |
| Quality inspection | Film contact and wrinkles | Film should contact the load consistently; minor wrinkles may be acceptable, but loose zones and large unrestrained pockets are not | Perform a four-side visual inspection after packaging | Identifies areas with insufficient containment before dispatch |
| Quality inspection | Pallet movement test | Set an internal pass/fail limit for visible product movement and load tilt based on the distribution route | Use a controlled manual push check or approved dynamic test procedure | Confirms that the completed package is stable for planned handling |
| Performance monitoring | Packaging defect rate | Track tears, loose hoods, unstable loads, and rework by product type and machine setting | Record defects per production batch or per 100 pallets | Provides measurable feedback for film, pattern, and parameter optimization |
| Transport preparation | Route and handling conditions | Account for forklift impacts, vibration, braking, stacking, temperature, moisture, and storage duration | Classify routes by handling severity and validate with representative shipment tests | Aligns packaging performance with actual distribution risks |
| Continuous improvement | Material-use efficiency | Reduce film consumption only after stability and damage results remain acceptable | Compare film mass per pallet with defect, damage, and rework data | Supports lower packaging waste without sacrificing load security |
Stretch hood film works best when containment begins with a balanced pallet, not excessive film tension. Before application, align cartons, remove damaged boxes, and keep the load within the pallet footprint. Uneven corners create pressure points, while empty gaps invite shifting during braking, turning, or vibration. Measure the load height and width, then choose a hood that fits without dragging across sharp edges. Small details matter.
During application, center the hood over the pallet and lower it evenly on all sides. Heat or mechanical stretching should follow the film supplier’s specified range and equipment settings. Too little tension allows movement; too much tension can crush soft cartons or distort unstable stacks. Use corner protection when edges are brittle, and inspect the bottom seal after wrapping. Do not trust appearance alone. Press lightly against several cartons and check whether the stack rebounds or leans.
Containment testing should mirror real handling conditions. Move sample pallets over ramps, turns, and short stops before approving a packaging setup. Record carton movement, film tears, and pallet deformation, not merely whether the load arrives intact. A practical target is stable contact across the load, with no visible gaps after testing. However, this target can mislead. A dense load may need less film than a tall, mixed carton stack. Our early assumption that tighter wrapping always meant safer transport proved incomplete. Recheck settings after seasonal temperature changes, new carton sizes, or operator adjustments.
Applying Stretch Hood Film for Balanced Load Containment
The chart compares common nominal pallet footprints used in logistics. Matching the stretch hood film width and sealing geometry to the pallet footprint helps maintain even tension around the load, reduce unsupported edges, and improve containment during handling and transport. Dimensions are shown in millimetres; actual pallet specifications may vary by region and application.
How to Optimize Pallet Stability with Stretch Hood in 2026?
Testing Pallet Stability and Improving Packaging Performance
A stable pallet begins with measured testing, not visual confidence. In warehouse trials, inspect the load after wrapping, handling, vibration, and short-distance transport. Record product movement, film tears, leaning corners, and pallet overhang. A stretch hood should grip the load evenly without crushing fragile cartons. Test several film tensions and hood sizes, because one setting rarely suits every pallet pattern. Measure the top load shift in millimeters after each trial. Small movement can become serious during repeated handling.
Tips: Use a repeatable test plan. Photograph every damaged corner. Mark the pallet’s centerline before testing. Compare results at different temperatures, since cold film can behave differently. Check the lower layers carefully; they often hide compression damage. Keep test records with load height, weight, film properties, and machine settings. These details make packaging decisions more reliable.
Do not rely only on a successful warehouse test. Add incline and vibration testing when transport conditions demand it. A pallet may look secure but still slide internally. We once accepted a configuration too quickly; later testing exposed weak restraint near the top layer. That mistake showed the value of challenging “good enough.” Review results with operators and quality staff, then adjust the hood’s overlap, tension, or pallet pattern. Better performance usually comes from small, verified changes.
Measure pallet width, height, weight, and center of gravity. Check the widest footprint. Note whether the load is tall, dense, mixed, or uneven.
A tall pallet with a narrow base needs stronger vertical restraint. A low, dense pallet may need less material. It still needs edge protection.
Mixed cartons can shift differently during braking, turning, and vibration. Soft bags may deform. Empty gaps can become movement paths.
Use enough tension to hold the top layer firmly. Excessive tension may crush soft cartons or distort unstable stacks. Tighter is not always safer.
Center the hood over the pallet. Lower it evenly on every side. Keep the load inside the pallet footprint and avoid sharp edges.
Inspect the bottom seal, film tears, carton deformation, and corner movement. Press several cartons lightly. They should rebound without leaning.
Test ramps, turns, short stops, forklift handling, and long-distance vibration. Horizontal acceleration near 0.5 g can expose weak stacking patterns.
No. Warehouse routes may contain rough floors or sudden turns. A perfect test result can still fail during real transport.
Cold storage can reduce film flexibility. Recheck settings after seasonal changes, new carton sizes, or operator adjustments. We once ignored this.
Do not judge stability by weight or appearance alone. A light pallet can shift badly. Record the strongest and weakest load patterns.
How to optimize pallet stability using stretch hood technology begins with understanding the load’s weight, dimensions, shape, center of gravity, and sensitivity to pressure or moisture. Selecting the appropriate film strength, elasticity, size, and protective properties helps ensure that the hood matches the pallet and product requirements. Before packaging, pallets should be clean, level, and structurally sound, while products must be aligned evenly with minimal gaps and stable stacking patterns. Corners, edges, and uneven layers may require additional attention to prevent movement during handling.
During application, the stretch hood should be positioned evenly and drawn down with balanced tension across all sides, avoiding excessive force that could damage products or weaken the film. After packaging, stability should be evaluated through visual inspection, movement checks, and controlled handling or transport simulations. Results can guide adjustments to film specifications, pallet arrangement, tension settings, and packaging procedures, improving containment, reducing shifting, and supporting safer, more efficient pallet performance in 2026.
